Our Products

Precision Injection Molding Solutions

From automotive interiors to EV charging infrastructure, we deliver high-precision injection molding solutions tailored to your industry needs. With over 19 years of expertise and IATF 16949 certification, we ensure quality at every step.

500+ Projects Delivered
50+ Global Partners
MOTORCYCLE INSTRUMENT CLUSTER TOOLING

Motorcycle Instrument Panel Injection Mold

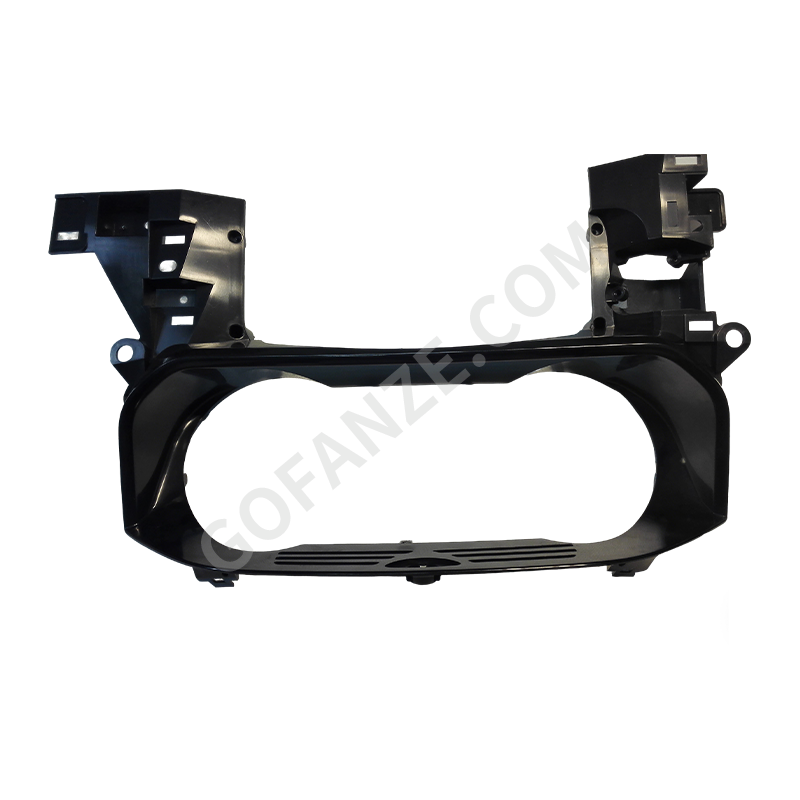
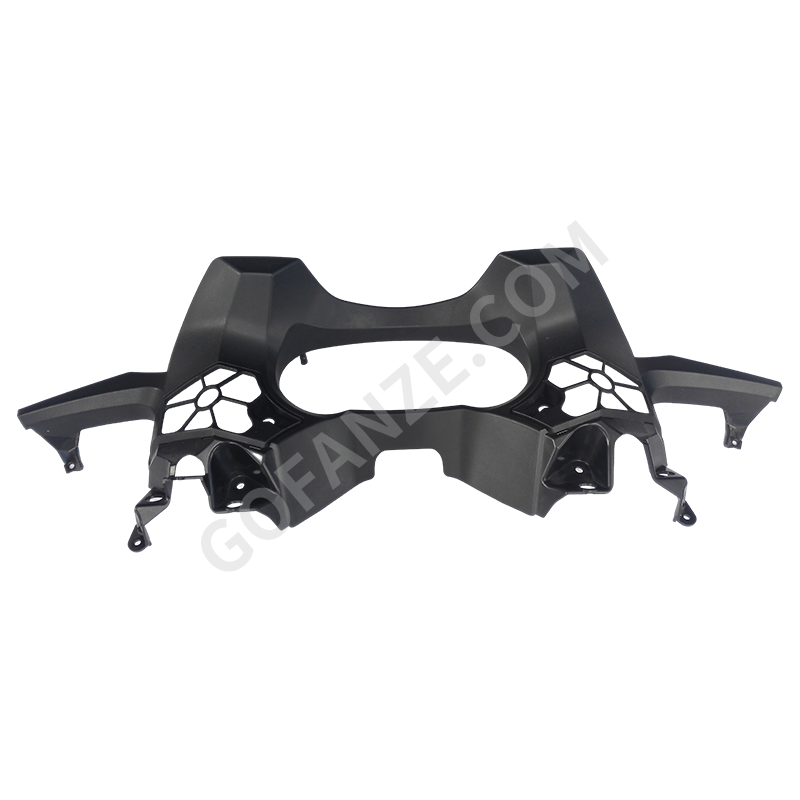
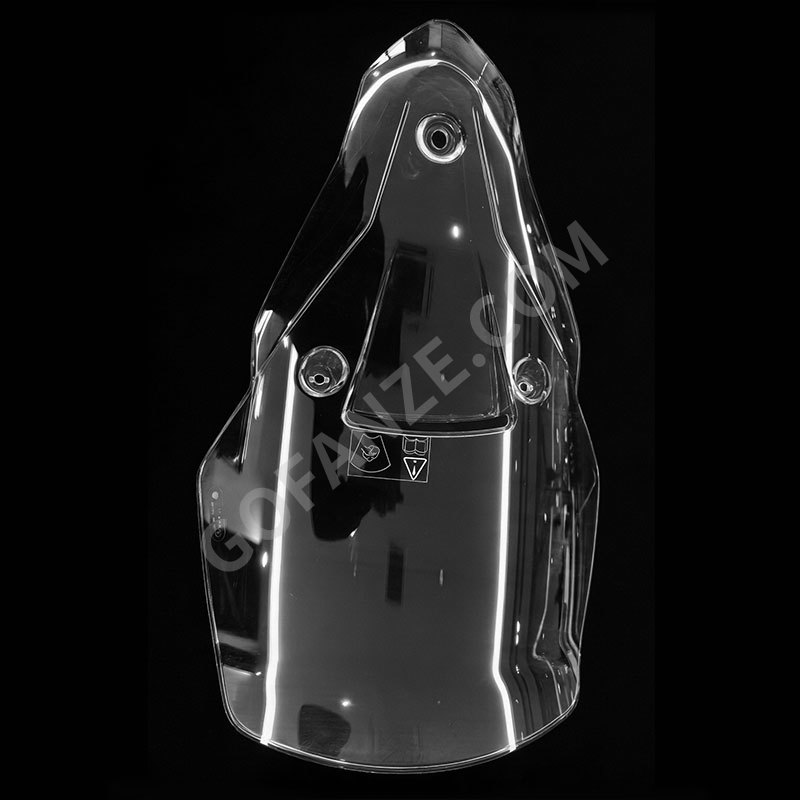
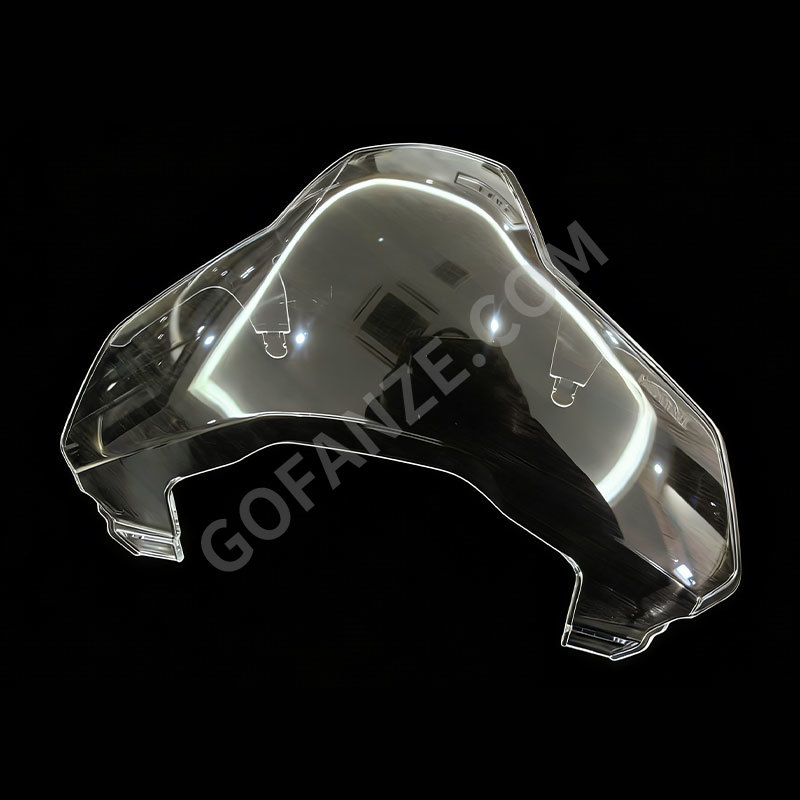
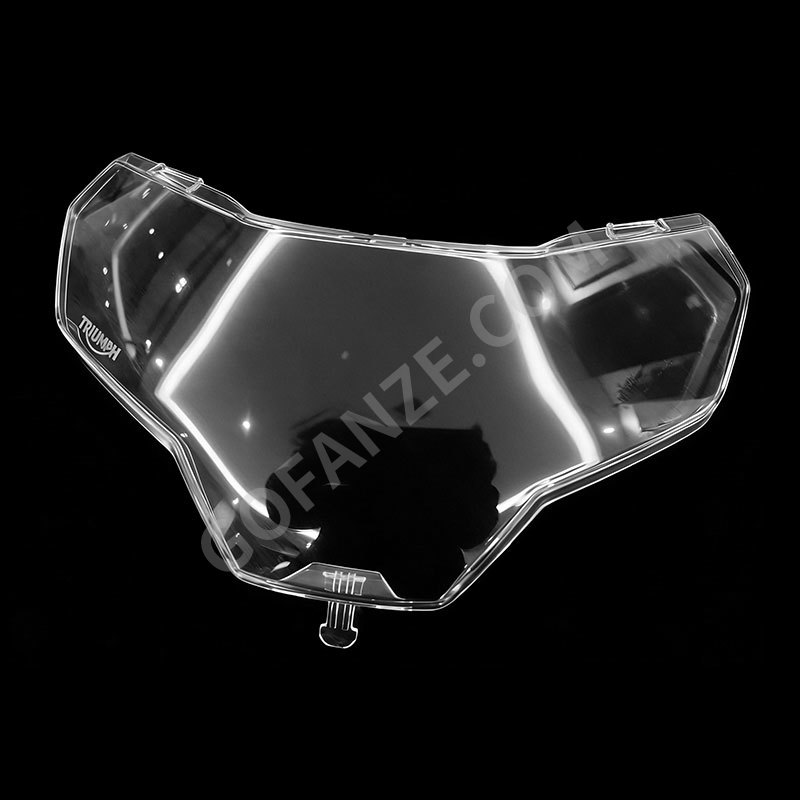
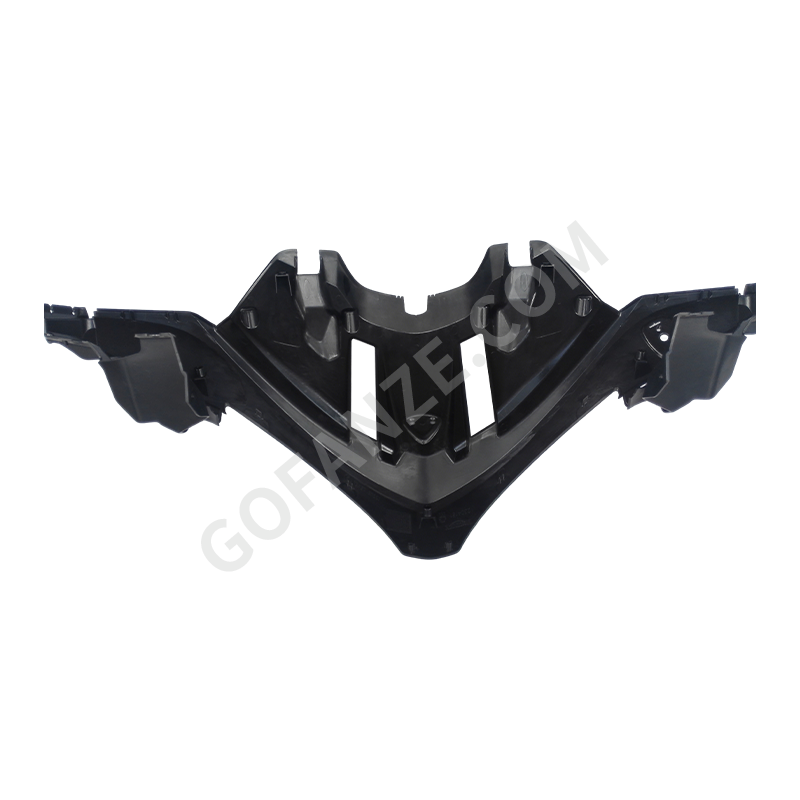
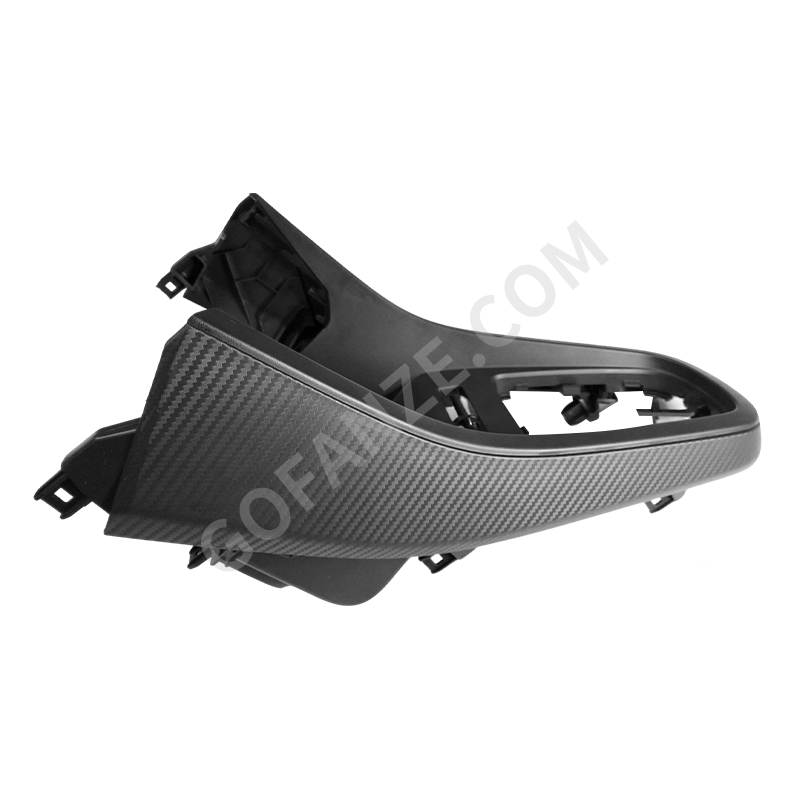
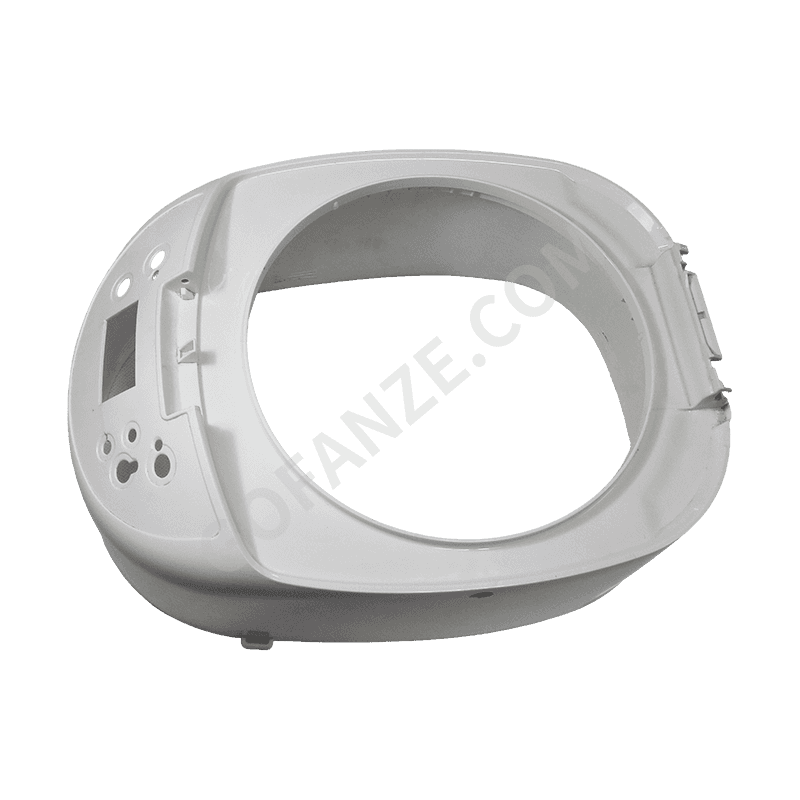
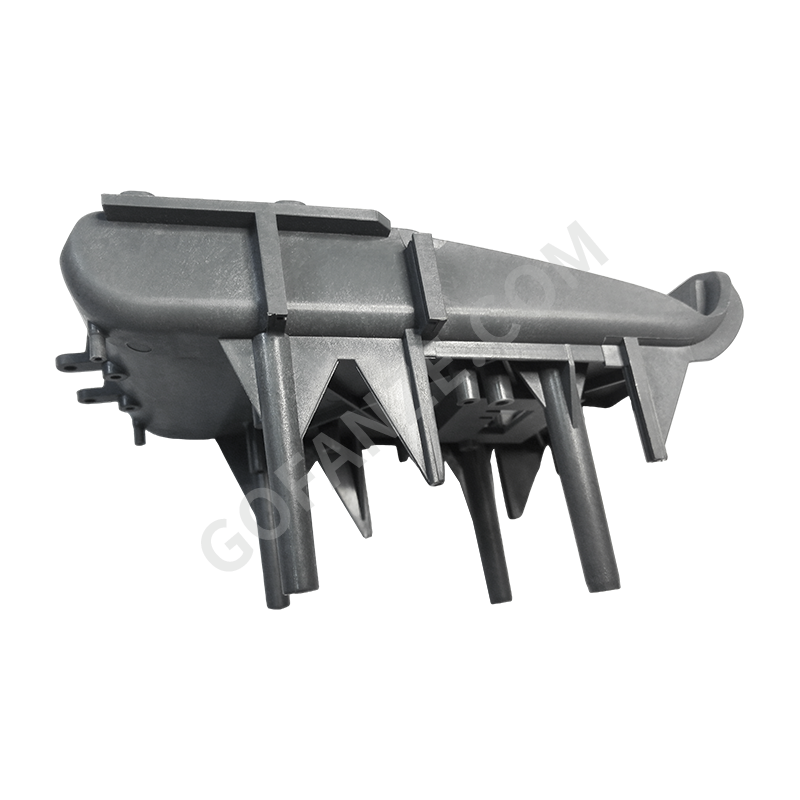
Production tooling for instrument panel covers, cluster housings, lens windows, gauge bezels, and switch panel frames. Engineered for optical clarity, UV stability, vibration resistance, and PC / PMMA / ABS material systems used in two-wheeler cockpit assemblies.

Optical Clarity UV Stabilized Vibration Tested
1000 max tonnage
1M shots life
48 day lead time
01 Overview
02 Capability
03 Parameters
04 Workflow
05 Quality
06 FAQ
Program Overview

Motorcycle instrument panel molds are built for manufacturing cockpit components that must satisfy optical clarity, UV aging resistance, vibration endurance, and dimensional consistency. Tooling is developed from customer CAD data with wall thickness verification, gating strategy, warp prediction, and optical surface validation before steel procurement. Molds accommodate PC, PMMA, ABS, and PC/ABS grades with dedicated polishing of lens and window surfaces to optical grade. Deliverables include DFM reports, mold flow analysis, steel certificates, T1 sampling, dimensional inspection reports, optical surface measurement data, and PPAP documentation packages suitable for two-wheeler OEM and Tier 1 cockpit suppliers.

Tooling Scope
Single & multi-cavity Family tooling 2K / overmold Insert molding
Materials
PC, PMMA ABS, PC/ABS PP+GF, PA+GF UV-stabilized grades
Tool Steel
P20 / 1.2311 H13 / 1.2344 Stavax ESR Nitriding / PVD
Deliverables
DFM report Mold flow analysis FAI / CMM report PPAP package
Technical Parameters
Mold base standard DME / HASCO / FUTABA / LKM
Clamping force range 150 – 1000 ton
Cavity quantity 1 – 8 (panel dependent)
Surface finish SPI A1, SPI A2, VDI 3400, texture
Hot runner Valve gate / open gate / sequential
Cooling Conformal circuits / baffles / bubblers
Ejection Pins + air poppets + stripper plate
Dimensional tolerance ±0.03 – ±0.10 mm (part dependent)
Optical surface tolerance ±0.02 mm on lens and window surfaces
Tool life 500k – 1M shots
Program Workflow
01
DFM & Quotation
Part review, wall thickness check, gate proposal, tonnage estimate
02
Mold Design
3D design, flow simulation, warp prediction, optical surface layout
03
Steel & Machining
CNC, EDM, wire cut, grinding, optical polishing, texture etching
04
Trial & Validation
T1 sampling, dimensional report, optical check, process tuning
05
Delivery & Support
PPAP package, spare parts, hot runner service, ramp-up support
Quality Control Points
Steel certificate and hardness verification
CMM dimensional inspection on cavity blocks
Mold flow simulation report before steel cutting
First article inspection with full dimension report
Optical surface roughness and clarity verification
Water circuit pressure and flow testing
Hot runner temperature uniformity validation
Final sample inspection against customer master
Procurement FAQ
Q What data is required to quote an instrument panel mold?
3D part data (STEP / IGES / native CAD), 2D drawing with tolerance and datum scheme, material specification including optical grade and UV stability, annual volume forecast, lens or window requirements, machine tonnage available, and target cycle time if defined.
Q What is the typical lead time for instrument panel tooling?
Standard lead time is 40–50 days for single-cavity cluster housings and 50–70 days for multi-cavity tools or panels with optical inserts, complex slide systems, and overmold requirements. Lead time begins after design freeze and includes T1 sampling.
Q How are optical windows and lens surfaces controlled?
Lens and window surfaces are machined and polished to SPI A1 or SPI A2 finish with surface roughness verified by profilometer. Optical inserts use Stavax ESR or equivalent steel with dedicated polishing sequences and protective handling throughout assembly and trial.
Q How is vibration resistance addressed in panel tooling?
Wall thickness and rib structures are validated during mold flow simulation to reduce resonance points. Mounting boss and clip geometry are dimensionally verified on T1 samples, and material selection targets impact-modified PC/ABS grades when vibration endurance is specified.
Q What after-sales support is provided?
Support includes remote process troubleshooting, spare parts supply, wear insert replacement, hot runner service, optical surface restoration, and on-site technical assistance for production ramp-up when required.
Request an instrument panel tooling quotation
Send part data, material specification, and volume forecast to receive DFM feedback and pricing within 48 hours.
Submit RFQ
Fanze T&M
| Precision Molding
IATF 16949 Since 2005
Precision Since 2005

Injection Molding Excellence

Singapore precision technology · 100+ experts · 21 export countries · IATF 16949 certified

100+
Team
21
Countries
24/7
Quick Response

Precision Mold
Development & Manufacturing

Fanze T&M (Jiashan) Co., Ltd. formerly known as Shanghai Fanze Precision Mould Co., Ltd., was founded in 2005 and specializes in the development of injection moulds and the manufacture of injection parts. We are China Motorcycle Instrument Panel Injection Mold Manufacturers and Custom Motorcycle Instrument Panel Injection Mold ODM/OEM Suppliers The company inherits Singapore's precision mold manufacturing technology.

In 2016, the company moved to Guigu Park, Jiashan, Zhejiang, with a plant area of 7,000 m² (usable 14,000 m²) and approximately 100 employees. Equipped with imported CNC, EDM, wire cutting, and high-performance injection molding machines from Japan and Germany.

Facility
14,000 m² · 100+ employees
Certification
IATF 16949 · ISO 9001
Founded
2005 · 19+ years of excellence

Advanced Equipment & Engineering

Full-service integration from development to assembly

[G]
Precision Tooling
Singapore technology with imported CNC, EDM & wire cutting
[F]
Injection Molding
Japanese & German machines, 14,000 m² facility
[Q]
Quality Assurance
IATF 16949 certified, rigorous quality control system
[I]
Integrated Manufacturing
Development · molding · printing · assembly

Trusted by Global Leaders

Land Rover Triumph SAIC Changan ABB Tiger Electric
Export
21+
Countries Worldwide
Japan · Europe · Americas · Southeast Asia
Quality Policy
"Precision, High Efficiency, Casting Quality"
Advanced equipment · Leading technology · Excellent team · Considerate service
Contact Us
Let's Talk
We'll respond within 24 hours
[N] *
[E] *
[P]
[M]